
Top Gate Valve Manufacturer Shijiazhuang Hanqian Technology Advances Industrial Valve Solutions
News originally published by
EIN Presswire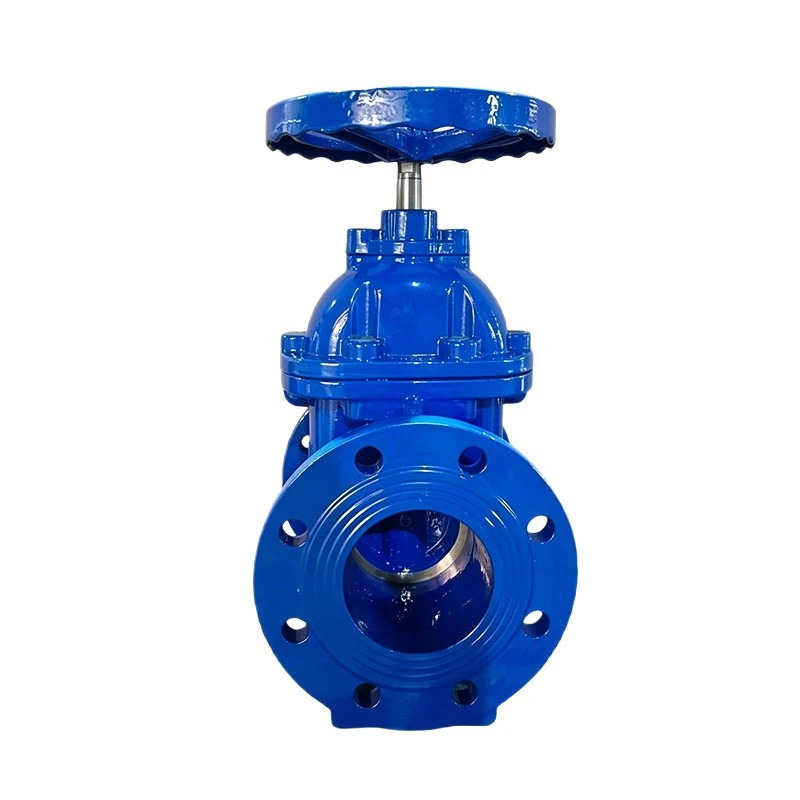
Cast Iron Non-Rising Stem Flanged Gate Valve
SHIJIAZHUANG, HEBEI, CHINA, November 20, 2026 /EINPresswire.com/ --
The global industrial valve market continues to develop as infrastructure investment, water management projects, energy production, and industrial manufacturing create growing demand for dependable fluid control equipment. Within this evolving market, Shijiazhuang Hanqian Technology Co., Ltd. is gaining attention as a supplier of industrial valve products, offering solutions designed to support different pipeline requirements. As industries place greater emphasis on operational reliability, product adaptability, and long-term equipment performance, the role of experienced gate valve manufacturers and suppliers has become increasingly important.
Gate valves remain essential components in industrial pipeline systems because of their ability to regulate the movement of liquids and gases through controlled opening and closing operations. Commonly used in water supply networks, oil and gas transportation, chemical processing, power generation, and general industrial facilities, these valves provide a practical solution for applications requiring reliable isolation. Their straightforward operating principle and adaptable structural designs have helped maintain their position as important equipment in modern fluid transportation systems.
Shijiazhuang Hanqian Technology Co., Ltd. participates in this competitive market by providing valve products that address various industrial and commercial requirements. With an emphasis on valve solutions and product availability, the company serves as a potential sourcing partner for buyers seeking equipment for pipeline construction, industrial maintenance, and fluid control applications. Its product range includes different valve categories, allowing customers to consider multiple options when developing or upgrading pipeline systems.
The Importance of Gate Valves in Modern Industrial Applications
Gate valves are widely recognized for their ability to provide effective shut-off functions in pipeline installations. Unlike regulating valves designed for continuous flow adjustment, gate valves are primarily intended to operate in fully open or fully closed positions. When completely open, the gate moves away from the main flow passage, allowing fluid to pass through with relatively little obstruction. When closed, the gate moves into position to block the passage and isolate the downstream pipeline.
This operating principle makes gate valves particularly useful in systems where dependable isolation is a priority. Municipal water distribution networks, industrial processing facilities, power plants, and oil transportation infrastructure frequently require valves capable of handling repeated operating cycles and varying service conditions.
For industrial buyers, selecting an appropriate gate valve involves evaluating several technical factors. These include operating pressure, temperature range, fluid characteristics, connection type, valve body material, sealing structure, and installation requirements. The selection process also needs to consider maintenance accessibility and compatibility with existing pipeline equipment.
Manufacturers and suppliers that understand these requirements can help customers identify suitable products for different operating environments. Shijiazhuang Hanqian Technology Co., Ltd. operates within this broader industrial supply landscape, where product variety and application suitability are important considerations for international procurement.
Material Selection and Manufacturing Considerations
Material selection is one of the most important aspects of valve manufacturing. Different pipeline environments expose valves to varying levels of pressure, temperature, corrosion, and mechanical stress. Consequently, the materials used for valve bodies, internal components, stems, and sealing elements can influence overall performance and service life.
Cast iron and ductile iron are commonly considered for water distribution and general utility applications. Carbon steel is frequently selected for industrial environments involving higher operating pressures and temperatures, while stainless steel is often used when corrosion resistance is an important requirement. The final choice depends on the characteristics of the transported medium and the conditions under which the valve will operate.
Manufacturing precision is equally important. Valve body dimensions, machining accuracy, surface finishing, and component alignment all contribute to the reliability of the finished product. In particular, the contact surfaces between the gate and valve seat must be appropriately designed to support effective sealing.
Quality inspection also plays a significant role in the production process. Depending on the applicable product specifications and standards, inspections may include dimensional verification, pressure testing, sealing performance evaluation, and visual examination. These procedures help identify manufacturing defects before products enter service.
For international buyers, understanding a supplier's manufacturing capabilities and quality management procedures is an important part of procurement. Specifications, testing documentation, material information, and relevant certifications should be reviewed before selecting valves for critical installations.
Complementary Valve Products for Pipeline Systems
Although gate valves provide essential isolation functions, industrial pipeline systems generally require several types of valves to achieve comprehensive flow management. Different operating conditions call for different valve structures, particularly when systems need to control flow direction, prevent reverse flow, or provide rapid shut-off capabilities.
Shijiazhuang Hanqian Technology Co., Ltd. offers products across multiple valve categories, including Ball Valve and Check Valve solutions. These products serve different purposes and can complement gate valves in a wide range of pipeline configurations.
Ball Valve products are widely used in applications requiring straightforward operation and effective flow shut-off. Their operating mechanism generally involves a rotating ball with a central passage. When the passage aligns with the pipeline, fluid can flow through the valve. A quarter-turn rotation moves the ball into a closed position, blocking the flow.
This relatively simple operating mechanism makes ball valves attractive for water systems, industrial equipment, chemical processing, and various utility installations. Depending on the design, materials, connection configuration, and sealing components, ball valves can accommodate different service requirements.
For procurement professionals, important considerations include nominal diameter, pressure rating, body material, ball material, seat composition, and connection standards. Selecting an appropriate configuration helps ensure compatibility with the surrounding pipeline and operating environment.
Check Valve products provide another important function in industrial fluid transportation. Unlike manually operated isolation valves, check valves are generally designed to allow fluid to travel in one direction while preventing reverse flow. Their operation helps protect pumps, compressors, pipelines, and other equipment from potential damage caused by backflow.
Different check valve designs may be selected according to flow characteristics, installation orientation, pressure conditions, and system requirements. Common configurations include swing check valves, lift check valves, and other specialized structures.
In water supply networks, for example, check valves can help prevent water from flowing backward when pumps stop operating. In industrial processing systems, they can support the protection of equipment and help maintain the intended direction of fluid movement.
By offering Gate Valve-related solutions alongside Ball Valve and Check Valve products, Shijiazhuang Hanqian Technology Co., Ltd. provides buyers with several product categories to consider when sourcing pipeline components. The availability of complementary valve types can simplify supplier communication and create opportunities for more coordinated procurement.
Responding to Changing Industrial Procurement Requirements
Industrial procurement has become increasingly sophisticated as businesses seek suppliers capable of meeting technical, commercial, and logistical expectations. Price remains an important purchasing factor, but it is no longer the only consideration. Buyers are also evaluating product consistency, specification flexibility, communication efficiency, delivery arrangements, and after-sales support.
For international customers, supplier evaluation often begins with reviewing product catalogs and technical information. Clear descriptions of valve materials, dimensions, pressure ratings, connection configurations, and applicable standards help purchasing teams determine whether a product meets project requirements.
The ability to communicate effectively is another important factor. Industrial valve purchases frequently involve detailed technical discussions, particularly when customers need specific configurations or are sourcing equipment for existing pipeline installations. Suppliers that can respond clearly to technical inquiries may help reduce misunderstandings during the purchasing process.
Shijiazhuang Hanqian Technology Co., Ltd. is positioned within this international sourcing environment, where customers increasingly look for suppliers offering a range of valve products. Its presence in the valve supply market reflects the continuing demand for practical pipeline equipment across different industrial sectors.
The company can be considered by buyers comparing available valve solutions for infrastructure projects, industrial facilities, and general fluid transportation applications. As with any industrial procurement decision, customers should confirm the relevant technical specifications, available materials, applicable certifications, and delivery arrangements before placing orders.
The Role of Quality Assurance in Valve Performance
Quality assurance is a fundamental consideration throughout the industrial valve supply chain. Even a well-designed valve may experience operational problems if its components are manufactured inaccurately, assembled incorrectly, or selected without sufficient consideration of the working environment.
For gate valves, sealing performance is particularly important because the primary purpose of the equipment is to isolate pipeline sections. Improper machining, unsuitable materials, or inadequate assembly can affect the contact between the gate and seating surfaces. These issues may lead to leakage or reduced operating reliability.
Ball valves also require careful attention to component precision. The ball, seats, stem, and sealing elements must work together to provide the intended shut-off performance. Similarly, check valves depend on appropriate internal movement and sealing arrangements to prevent unwanted reverse flow.
Pressure testing is an important inspection method for industrial valves. Depending on the relevant design standard and product requirements, testing may evaluate the strength of the pressure-containing body and the sealing performance of the closed valve. Dimensional inspections and material verification can provide additional information about product conformity.
For buyers working with Shijiazhuang Hanqian Technology Co., Ltd., reviewing available quality documentation and confirming the applicable testing requirements can help establish a clearer understanding of product suitability. This is particularly relevant for projects involving demanding operating conditions or strict engineering specifications.
Market Opportunities and Future Development
The outlook for the industrial valve sector remains closely connected to developments in infrastructure, energy, manufacturing, and environmental management. Urban expansion continues to create demand for water distribution and wastewater treatment facilities, while industrial modernization requires reliable components for increasingly complex production systems.
The development of energy infrastructure is another important market driver. Oil and gas transportation, chemical processing, power generation, and related industries all depend on valves to control and isolate fluids under different operating conditions.
At the same time, customers are paying greater attention to equipment efficiency, maintenance costs, and operational safety. These priorities are encouraging suppliers to focus on product consistency, technical communication, and solutions that address specific application requirements.
Digitalization is also influencing industrial procurement. Online product catalogs, digital technical documentation, and more efficient communication channels are making it easier for international buyers to compare suppliers and evaluate available products. Companies with accessible product information can improve the purchasing experience and help customers make more informed decisions.
For valve suppliers, maintaining competitiveness requires a combination of product knowledge, manufacturing coordination, quality awareness, and customer service. Companies that understand the changing requirements of industrial buyers will be better positioned to participate in international supply chains.
Shijiazhuang Hanqian Technology Co., Ltd. operates in a market where these factors continue to shape purchasing decisions. By offering multiple valve product categories, including gate valves, ball valves, and check valves, the company addresses several common requirements within industrial pipeline systems.
Conclusion: Supporting Reliable Industrial Fluid Control
Gate valves continue to play an important role in industrial infrastructure because of their practical isolation capabilities and broad application potential. As pipeline networks become more extensive and industrial systems require increasingly dependable components, selecting suitable valves remains a critical part of project planning and equipment procurement.
The complementary functions of ball valves and check valves further demonstrate the importance of selecting appropriate equipment for different stages of fluid transportation and control. Each valve type serves a distinct purpose, and successful system design depends on matching product characteristics with actual operating conditions.
Shijiazhuang Hanqian Technology Co., Ltd. is among the companies participating in this evolving valve supply market. Through its range of valve products and focus on industrial pipeline applications, the company provides international buyers with additional options when evaluating fluid control equipment.
As global demand for dependable pipeline components continues, manufacturers and suppliers that emphasize product suitability, consistent quality, and effective customer communication will remain important participants in the industrial valve industry.
Company Profile: Shijiazhuang Hanqian Technology Co., Ltd.
Shijiazhuang Hanqian Technology Co., Ltd. is a China-based company operating in the industrial valve sector. Located in Shijiazhuang, Hebei Province, the company participates in the supply of valve products for customers involved in industrial applications, pipeline construction, infrastructure development, and fluid transportation.
Its product portfolio includes Gate Valves, Ball Valves, Check Valves, and other valve-related products designed for different pipeline configurations and operating requirements. These product categories address common industrial needs involving flow isolation, shut-off operations, and reverse-flow prevention.
The company serves buyers looking for valve sourcing options and product configurations suitable for different applications. Customers can consult the company's product information to learn more about available valve categories and identify products that correspond to their technical and procurement requirements.
For additional company and product information, visit the official website: www.hqvalvetech.com.
Address: No.259, West 2nd Street, 2nd Floor, Hall 3, Lecheng International Trade City, No.36 Tianshan North Street, Chang'an District, Shijiazhuang, Hebei Province
Official Website: https://www.hqvalvetech.com/
Han Weigeng
Shijiazhuang Hanqian Technology Co., Ltd.
weigenghan@gmail.com
Legal Disclaimer:
EIN Presswire provides this news content "as is" without warranty of any kind. We do not accept any responsibility or liability for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this article. If you have any complaints or copyright issues related to this article, kindly contact the author above.
